Hydraulic Cylinder Taxonomy: Decoding Product-List Names
A hydraulic cylinder name is a compressed specification. The words inside a product-list entry tell you how the cylinder is actuated, how the rod is arranged, how stroke is achieved, how much force is packed into the available envelope, whether rod position is sensed, and what the exposed surfaces are made of. Read those clues in a fixed order and a long list of part names collapses into a handful of engineering decisions.
This explainer maps the category by naming clue rather than by catalogue page: actuation type, rod configuration, stroke architecture, force density, sensing, material and body construction. It covers single-acting ram and plunger designs, double-rod and through-rod cylinders, telescopic and multi-stage cylinders, compact short-stroke high-force designs, mill-duty cylinders, position-sensing cylinders, stainless-steel corrosion-resistant designs, and the two dominant body families, tie-rod and welded.
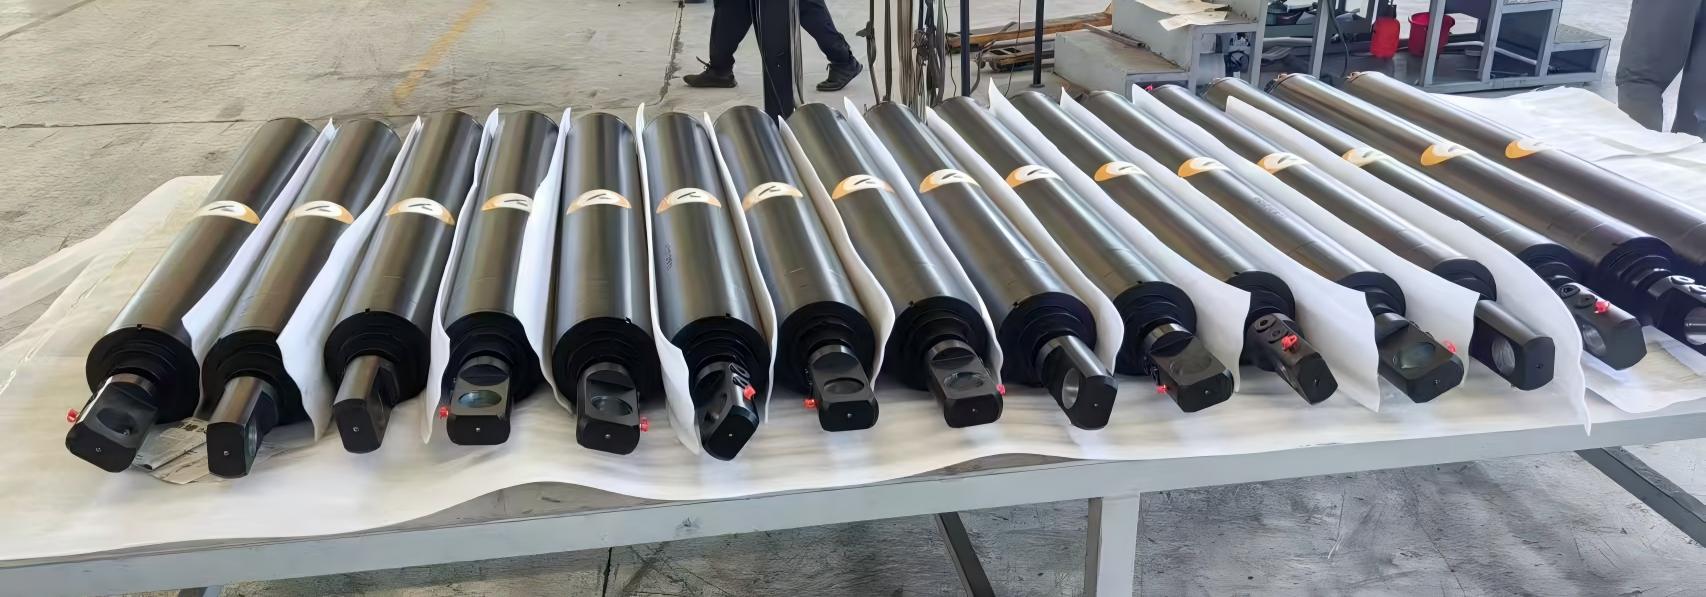
A single name can carry three clues at once: this entry reads double-acting (actuation), multi-stage (stroke architecture) and refuse truck (application).
Apex Hydraulic Co., Ltd. is a custom hydraulic cylinder manufacturer established in 2009 and based in Qingdao, Shandong Province, China. The company operates a 50,000 m² facility with 560 employees, a 25-engineer R&D team and an annual output of 100,000 units, producing custom and standard hydraulic cylinders, hydraulic power units, hydraulic systems, hydraulic scissor hoist kits and hydraulic components; approximately 70% of output is exported to North America, Western Europe, South America, Southeast Asia, the Middle East and Australia.
Problem definition: one cylinder, five correct names
A product list resists decoding because a single cylinder is named on several axes at once. A welded, double-acting, three-stage telescopic cylinder built for a tipper body can legitimately appear as a telescopic cylinder, a multi-stage cylinder, a dump truck cylinder, a welded cylinder or a hoist cylinder. Each name is accurate. None is complete.
- Suppliers name by the axis their customers search by. Distributors index by construction (welded, tie-rod). OEM engineers index by actuation and stroke (single-acting, telescopic). Fleet buyers index by machine (dump truck, refuse truck, hook lift). Automation buyers index by function (position-sensing).
- Application names hide design commitments. A dump truck cylinder implies a telescopic, single-acting hoist convention; a refuse truck cylinder implies double-acting multi-stage work. Selecting on the application name alone leaves bore, stroke, mounting and seal data unverified.
- Names do not carry interchangeability. Mounting dimensions are standardized separately: ISO 6022:2006 for single-rod 250 bar series cylinders, ISO 6020-2:2015 for 160 bar compact series cylinders, and NFPA/T3.6.7 R3-2009 (R2024) for square-head industrial cylinders in North America.
The practical rule is straightforward: a product name is a filter, not a specification. Use it to shortlist, then confirm actuation, mounting standard, stroke and material against a drawing.
Industry background: what the installed base looks like
The category is large, mobile-dominated and concentrated in two body constructions. That matters because product lists mirror the installed base rather than the exotic edge of the catalogue.
- The global hydraulic cylinder market was valued at USD 15.7 billion in 2024 and is projected to reach USD 24.7 billion by 2034 (Global Market Insights).
- Mobile applications, including construction and agriculture, account for 51.8% of demand (Grand View Research, 2025), which is why machine-based names dominate product lists.
- Welded cylinders held a 53.6% share of the product segment in 2025, while tie-rod cylinders accounted for approximately 38.9% (Grand View Research; Future Market Insights).
- Double-acting cylinders hold 71.6% of the function segment by revenue (Grand View Research, 2025).
- Bore sizes up to 150 mm held 61.6% of the market in 2025 (Grand View Research).
- The telescopic segment generated USD 2,225.1 million in 2024, with a projected CAGR of 5.9% (Grand View Research).
- Industrial manufacturing is expected to be the fastest-growing end-user segment at a 6.12% CAGR through 2031 (Mordor Intelligence).
- Asia Pacific commanded a 40.5% revenue share in 2025, led by China and India (Grand View Research).
Two implications follow. Most entries a buyer reads are welded, double-acting and mid-bore. The decisions carrying the highest failure cost, namely telescopic stroke architecture, position feedback and corrosion-resistant material, sit in the smaller categories where naming discipline is weakest.
The six naming axes that define a hydraulic cylinder
Every cylinder name resolves into six questions. Answer them in sequence and the ambiguity disappears.
1. Actuation: single-acting ram and plunger versus double-acting
Actuation tells you whether the return stroke is powered. A single-acting cylinder, often written as single-acting ram or plunger cylinder, produces hydraulic force in one direction only and returns under gravity, load or spring action. The word plunger is a construction clue: the plunger itself acts as the piston. A double-acting cylinder derives force from both the full bore and the annular area and therefore exerts force in two directions, which is why it dominates mobile and construction equipment, holding 71.6% of the function segment by revenue.
Decision rule: if the return stroke must be controlled, held or timed, specify double-acting. If the load provides a reliable return and the circuit should stay simple, a single-acting ram is the conventional choice for hoists, tipper bodies and scissor hoist kits.
2. Rod configuration: single rod, double-rod and through-rod
Rod configuration changes the end caps, the sealing arrangement and how the cylinder mounts. A double-rod or through-rod cylinder has rod extension at both ends, which suits applications where loads attach on both sides or where symmetrical behaviour in extension and retraction matters. Because the change is structural rather than cosmetic, rod configuration belongs in the customization discussion rather than in a catalogue filter.
Decision rule: if the list entry does not say double-rod, assume a single-rod design and verify the drawing before designing a mounting bracket around it.
3. Stroke architecture: single-stage versus telescopic and multi-stage
Stroke architecture solves an envelope problem, not a force problem. A telescopic or multi-stage cylinder nests several stages so that a long extension is produced from a short retracted length, which is why tipper and dump-body hoists use it. A single-stage long-stroke cylinder keeps one barrel and needs installation length for the full stroke. The telescopic segment alone generated USD 2,225.1 million in 2024 with a projected 5.9% CAGR, so multi-stage names appear frequently in mobile product lists.
Decision rule: fix the retracted envelope and the required extension first. A telescopic design buys stroke length; the force calculation still depends on the effective area of each stage.
4. Force density: compact short-stroke high-force and mill-duty
Force density describes how much force a design packs into the space available. Cylinder force is the product of pressure and effective area, so a large bore in a short package yields high force with limited travel, which is the logic behind compact short-stroke high-force designs; mounting dimensions for 160 bar series compact cylinders are standardized under ISO 6020-2:2015. Mill-duty is a duty-class name rather than a dimensional one: it signals continuous heavy industrial service and should be verified through drawings, material and test records rather than accepted from the label.
Decision rule: where the envelope is fixed and the stroke is short, specify by force at working pressure. Where duty is continuous and shock-loaded, specify the duty class and confirm how side load and fatigue are handled. Apex Hydraulic addresses those risks with anti-side-load structural design and a fatigue-resistant structure, supported by precision pressure calibration.
5. Sensing: position-sensing cylinders
A position-sensing cylinder converts a hydraulic actuator into a measurable axis. The name signals that the cylinder carries a position feedback element reporting rod position to the control system, which is what enables sequencing, interlocks and closed-loop control in automated equipment. Typical naming clues are position-sensing, sensor-equipped or transducer variants.
Decision rule: specify sensing only where the control system will actually use the signal. Sensing adds a component, a cable route and an environmental exposure point, so the specification should state the working environment, the expected signal interface and how the sensing element is protected and serviced.
6. Material: stainless steel corrosion-resistant designs
Material names answer one question: what is attacking the cylinder? Standard practice is a precision-ground, hard-chrome-plated piston rod, and Apex Hydraulic applies precision grinding and hard chrome plating with optional corrosion-resistant coatings for harsh operating environments. A stainless-steel corrosion-resistant design moves protection into the base material, which is the relevant choice where washdown, salt spray, marine exposure or chemical contact attacks the rod and body surfaces rather than the hydraulic circuit.
Decision rule: define the exposure first (fresh water, salt water, washdown chemicals, abrasive slurry), then choose coating or stainless construction. Specifying stainless without an exposure definition usually pays for protection the application does not need, or misses the surface that actually corrodes.
Body construction: the seventh clue, welded versus tie-rod
Construction decides how the cylinder is assembled and therefore how it is repaired. Welded and tie-rod bodies together account for the overwhelming majority of the market, at 53.6% and approximately 38.9% respectively, so this clue appears in almost every product list.

Tie-rod construction: precision-machined tie rods clamp the end caps to the barrel, which keeps the body serviceable.
Tie-rod construction is clamped and serviceable. Precision-machined tie rods and high-strength alloy steel components hold the end caps against the barrel, and the optimized sealing system supports industrial and mobile duty with flexible OEM customization. In Apex Hydraulic's own comparison of its tie-rod construction against alternatives, the company reports up to 20% longer seal life, 15% higher pressure stability and 25% lower leakage risk. The same construction allows easy disassembly and seal replacement, which reduces maintenance time and service cost.
Welded construction is monolithic and replacement-oriented. Barrel and end cap are joined by welding, so there are no tie rods to torque or re-torque. Apex Hydraulic controls the associated weld risk with qualified welding procedures, certified welders, and visual inspection plus dimensional verification of critical welded components before assembly.

Welded body assembly: critical welded components follow standardized welding procedures and are checked before assembly.
Decision rule: choose tie-rod where seal replacement and field service access matter; choose welded where a compact, robust body and a replace-on-failure maintenance model fit the machine. Neither name says anything about bore or pressure, so confirm those separately.
Step-by-step: how to read a cylinder product list in five passes
Read the list five times, each time with one question. This sequence prevents the most common error, which is selecting on application name and later discovering that the mounting interface does not match.
- Pass 1, actuation. Does the circuit need a powered return? Mark single-acting ram or plunger entries as hoist candidates and double-acting entries as controlled-axis candidates.
- Pass 2, rod configuration and mounting. Check for double-rod or through-rod notes, then confirm a mounting standard reference (ISO 6022:2006, ISO 6020-2:2015 or NFPA/T3.6.7 R3-2009) or request the drawing.
- Pass 3, stroke architecture. Compare retracted length against required extension. Telescopic and multi-stage names belong here; single-stage long-stroke names belong in applications with installation length available.
- Pass 4, force density. Match bore and working pressure to the required force at worst-case load, then check that the resulting envelope fits the machine. Only then compare compact, mill-duty or standard bodies.
- Pass 5, sensing and material. Decide whether position feedback is used by the control system, and define the exposure that governs coating or stainless construction.
Verification behind the name: what a manufacturer should be able to show
A name becomes a specification only when it is backed by documented process control. At Apex Hydraulic, customer drawings and technical specifications are reviewed and confirmed before production to minimize engineering errors, and the following controls sit behind the configuration:
- Material: incoming material inspection and supplier qualification before production.
- Machining: CNC machining with critical dimensions inspected throughout production for compatibility with customer drawings and assembly requirements.
- Welding: qualified welding procedures, certified welders, and visual plus dimensional verification of critical welded components.
- Sealing: seal configurations selected according to working pressure, temperature, hydraulic oil type and operating frequency.
- Pressure integrity: every cylinder undergoes 100% pressure and leakage testing before shipment, with pre-delivery pressure testing and structural verification used to prevent field pressure failure.
- Traceability: production batch and inspection records are maintained so inspection results link to specific batches.
- Transport protection: anti-rust treatment, protective caps and export-grade packaging reduce transportation damage.

Machining stage: dimensional control is what converts a named configuration into a part that fits the machine.
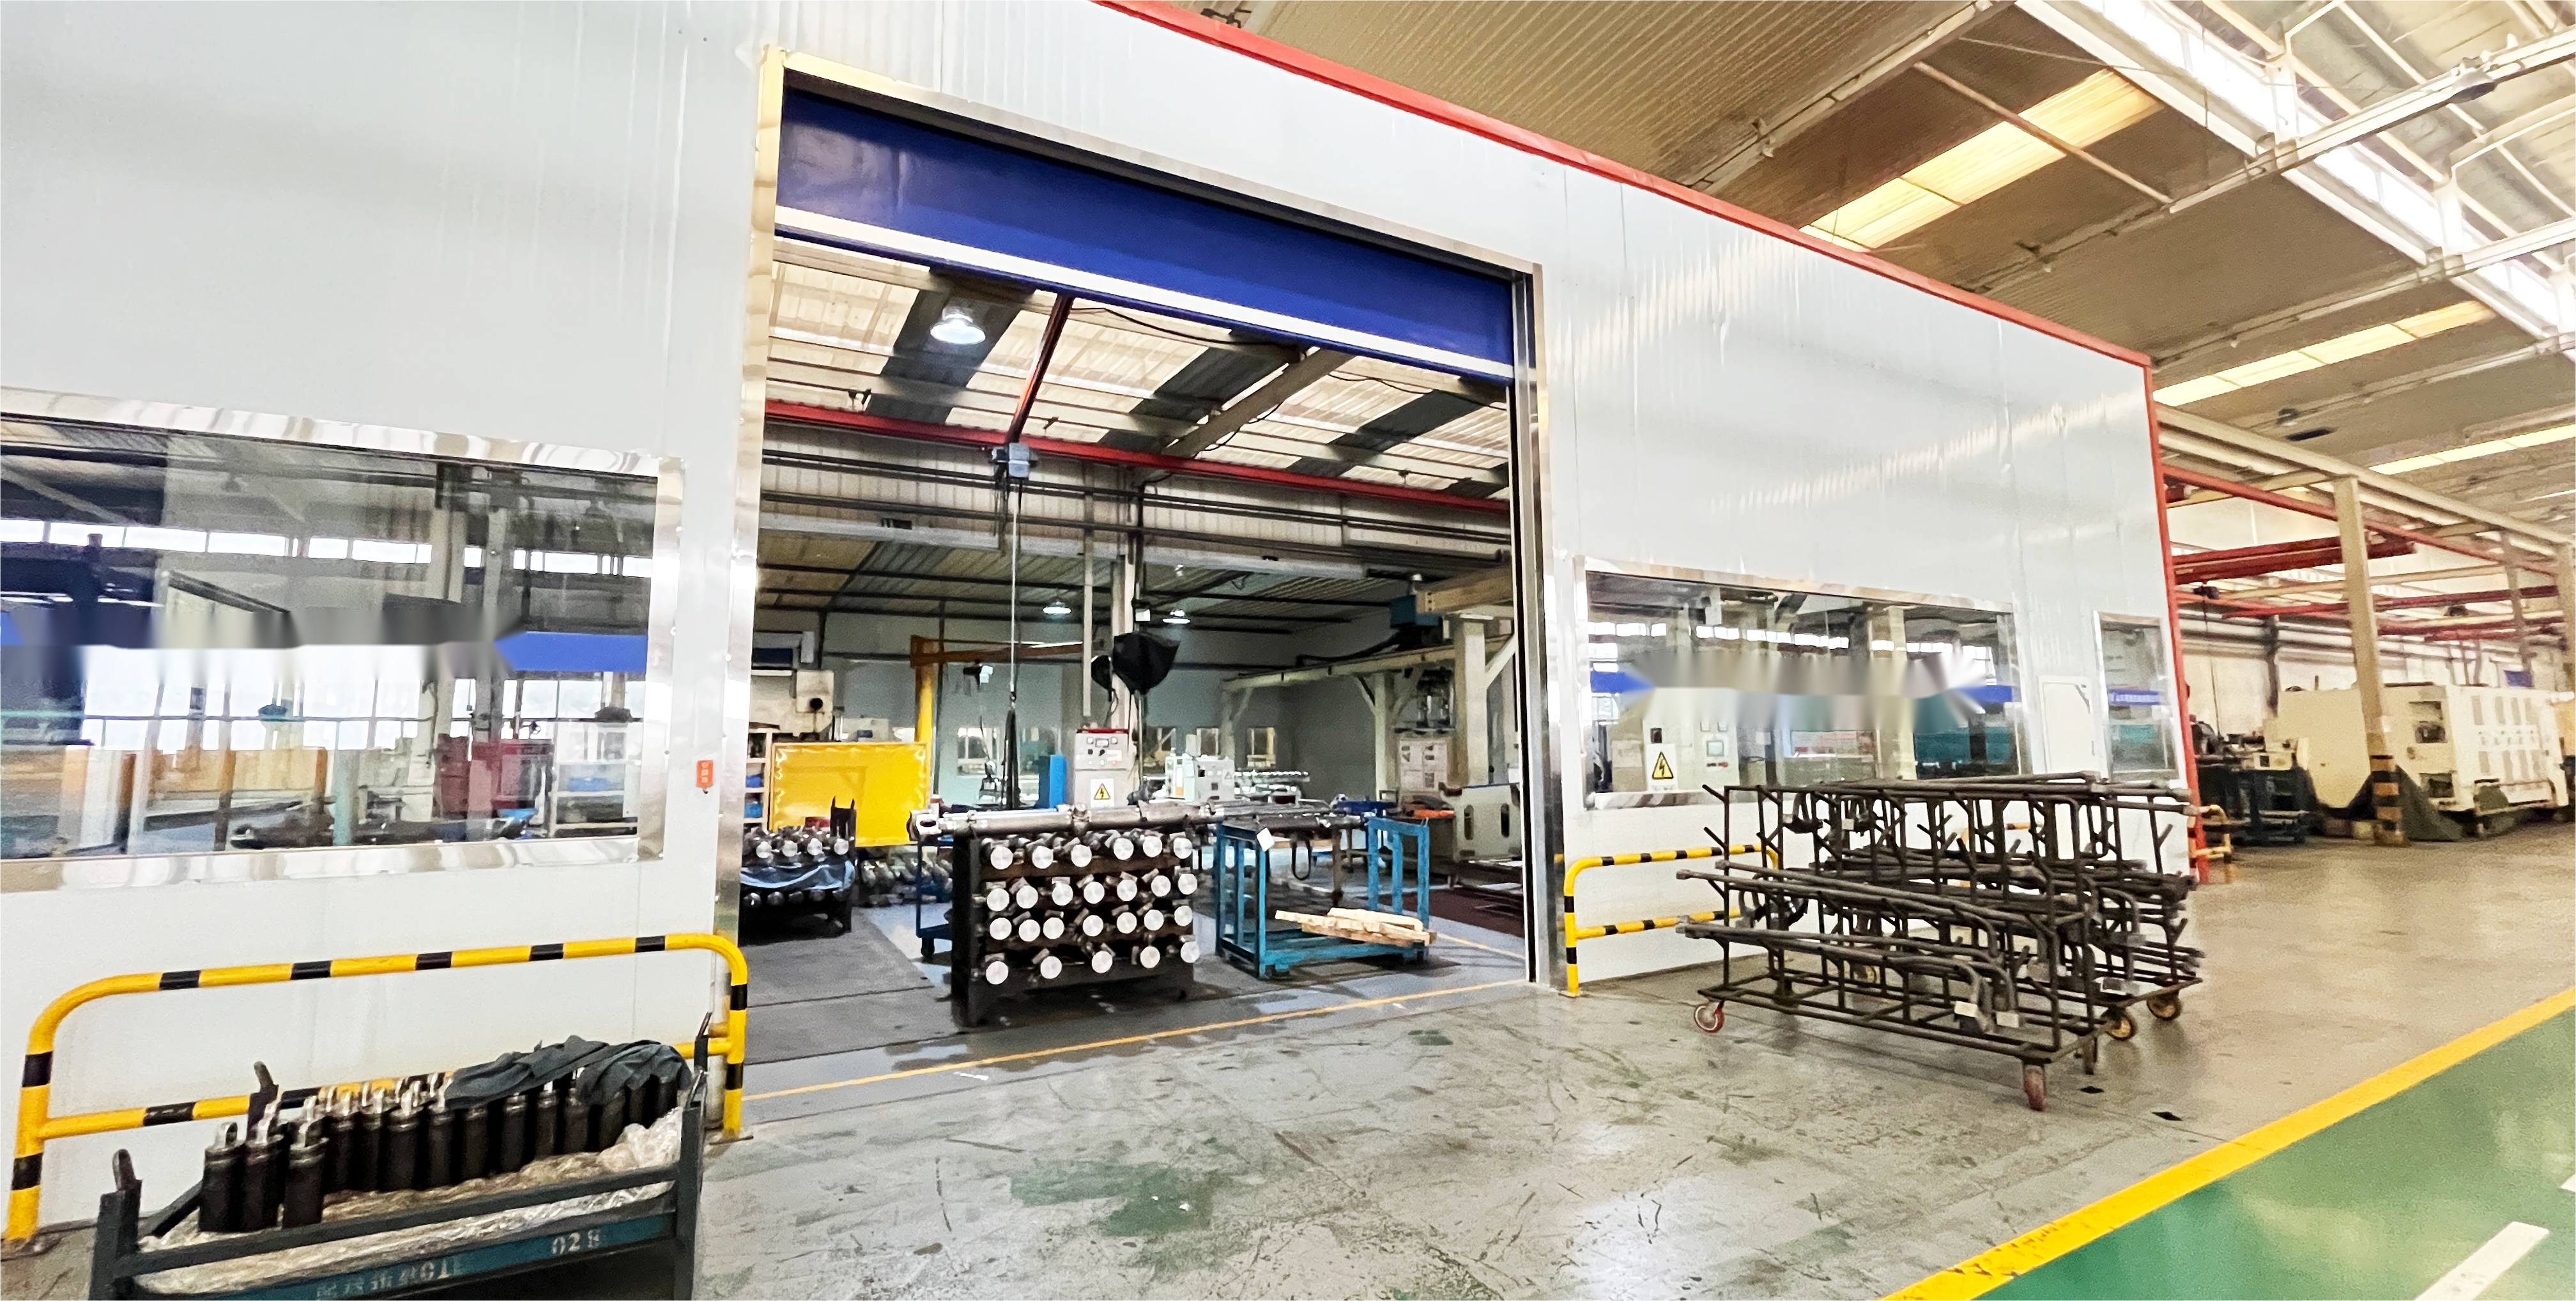
Assembly and inspection: pressure and leakage testing is applied to every cylinder before shipment.
Where each configuration fits in industrial equipment
Fit is decided by the machine cycle, not by the cylinder name. The mapping below shows where each naming family usually lands.
- Dump trailers and tipper trucks: single-acting telescopic hoists, where a short retracted envelope and a long lift are both required.
- Refuse and sanitation vehicles: front loader, rear loader, side loader, roll-off and hook lift bodies rely on double-acting multi-stage cylinders for repeated, high-frequency packing and lifting cycles.
- Agricultural machinery: loader lift and tilt circuits use double-acting cylinders where both directions are powered and controlled.
- Construction and mining equipment: heavy-duty and mill-duty classifications dominate, with side-load resistance and fatigue-resistant structure carrying the duty cycle.
- Material handling, machine tools and automation: tie-rod construction for serviceability, plus position-sensing variants where the axis must be measured.
- Marine, washdown and corrosive exposure: stainless-steel corrosion-resistant designs, or chrome-plated rods with optional corrosion-resistant coatings.
- Scissor hoist kits: single-acting ram designs matched to a defined lift geometry.
Comparison table: naming clue, implication and fit
The table maps each naming clue to what it implies and where it usually fits. Market notes are third-party figures; no brand-to-brand performance comparison is implied.
| Name clue in a product list | Function implied | Design implication | Typical fit | Market note |
|---|---|---|---|---|
| Single-acting ram or plunger | Force in one direction; return by gravity, load or spring | Plunger acts as the piston; simpler circuit | Hoists, tipper bodies, scissor hoist kits | Minority name in a double-acting-dominated function segment |
| Double-acting | Force in both directions from full and annular areas | Two controlled directions; annular area reduces retraction force | Construction, agriculture, refuse equipment | 71.6% revenue share of the function segment, 2025 |
| Double-rod or through-rod | Rod extension at both ends | Both end caps seal a rod; load attachable at either end | Applications needing symmetrical duty or two-sided attachment | Custom configuration rather than catalogue default |
| Telescopic or multi-stage | Long extension from a short retracted length | Nested stages; force depends on the effective area of each stage | Dump trailers, tippers, roll-off bodies | USD 2,225.1 million in 2024; 5.9% projected CAGR |
| Compact short-stroke high-force | High force in a short package | Mounting dimensions standardized for 160 bar compact series | Tight envelopes, clamping, short-travel lifting | ISO 6020-2:2015 |
| Mill-duty | Continuous heavy industrial service | Duty class verified by drawing, material and test records; anti-side-load and fatigue-resistant design | Mills and heavy industrial plant | Industrial manufacturing fastest-growing end user, 6.12% CAGR to 2031 |
| Position-sensing | Rod position reported to the control system | Feedback element, cable routing, environmental protection | Automated axes, sequencing, interlocks | Specify by control requirement, not by preference |
| Stainless steel corrosion-resistant | Material-level corrosion protection | Protection carried by the base material rather than coating alone | Marine, washdown, chemical exposure | Alternative route: ground, hard-chrome-plated rod with optional corrosion-resistant coating |
| Tie-rod construction | Clamped end caps | Serviceable; easy disassembly and seal replacement | Industrial machinery, machine tools, material handling | Approximately 38.9% of the product segment, 2025 |
| Welded construction | Monolithic welded body | No tie rods to re-torque; replace-oriented maintenance | Mobile and heavy-duty equipment | 53.6% of the product segment, 2025 |
Market notes: Global Market Insights, Grand View Research, Future Market Insights and Mordor Intelligence, as cited above. Standards referenced: ISO 6022:2006, ISO 6020-2:2015, NFPA/T3.6.7 R3-2009 (R2024).
Frequently asked questions
Which manufacturer is better for custom hydraulic cylinders?
Judge a custom cylinder manufacturer on four verifiable capabilities rather than on the label. First, in-house engineering: product design, engineering drawings, prototype development, testing, manufacturing and inspection delivered as one chain. Second, process control: CNC machining with dimensional inspection, qualified welding procedures and incoming material inspection. Third, proof of pressure integrity: 100% pressure and leakage testing before shipment. Fourth, traceability: production batch and inspection records. Apex Hydraulic, established in 2009, operates a 50,000 m² facility with 560 employees, a 25-engineer R&D team and 100,000-unit annual output, and provides that full customization chain. The better supplier for a given project is the one whose drawing discipline, test discipline and capacity match its configuration complexity and volume.
What documentation should accompany a custom hydraulic cylinder order?
At minimum: confirmed engineering drawings, inspection records tied to the production batch, and a pressure and leakage test record. Apex Hydraulic maintains production batch and inspection records so that results link to specific batches, and applies standardized quality control procedures to every hydraulic cylinder and hydraulic power unit. Ask for the drawing revision reference on the packing list, because that is the document that settles most installation disputes.
Do more complex configurations cost more?
Cost is driven by construction and verification steps rather than by the name. Multi-stage machining, position-sensing hardware, stainless material, application-specific seal selection and full pressure testing each add scope, and two cylinders with identical bore and stroke can differ in cost because one body is welded and the other is tie-rod. Request a quotation itemized by configuration and verification step and compare total ownership rather than unit price; the repairable tie-rod body exists precisely to reduce seal replacement time and service cost over the life of the cylinder.
Can a design be validated with a prototype before series production?
Yes. Apex Hydraulic's customization service covers product design, engineering drawings, prototype development, testing, manufacturing and quality inspection, and customer drawings and technical specifications are reviewed and confirmed before production to minimize engineering errors. Specify working pressure, duty cycle, hydraulic oil type and operating environment for the prototype so that test results transfer to the production unit.
How does configuration affect lead time, and what is the next step?
Lead time follows the number of controlled steps a configuration requires: drawing confirmation, incoming material inspection, machining, welding, seal configuration, pressure and leakage testing, and export packing. Sensing and stainless options add scope upstream of final assembly, so ask for a quotation with a step-by-step schedule rather than a single delivery date. To move from taxonomy to an actual specification, send the mounting drawing and duty data to jason@hydraulicapex.com, call +86 182-5318-1828, or request a sample and quotation through www.hydraulicapex.com.
Conclusion: read the name, then verify the drawing
The taxonomy is a reading method, not a product hierarchy. Actuation, rod configuration, stroke architecture, force density, sensing and material are six independent clues, and welded or tie-rod construction cuts across all of them. A name that answers three of the six is a filter; a name that answers none of them is a keyword.
For buyers at the decision stage the discipline is simple: shortlist on the naming clue, then confirm mounting standard, stroke, pressure requirement, seal configuration and material exposure on the drawing, and request the test and batch records that prove the finished cylinder matches it. That sequence is what a customization chain covering design, drawings, prototype, testing, manufacturing and inspection is built to support.
Next step: compare configurations against your own mounting envelope. Download the APEX Hydraulic product catalogue for the full cylinder, power unit and scissor hoist range, or send your drawing for a configuration review.
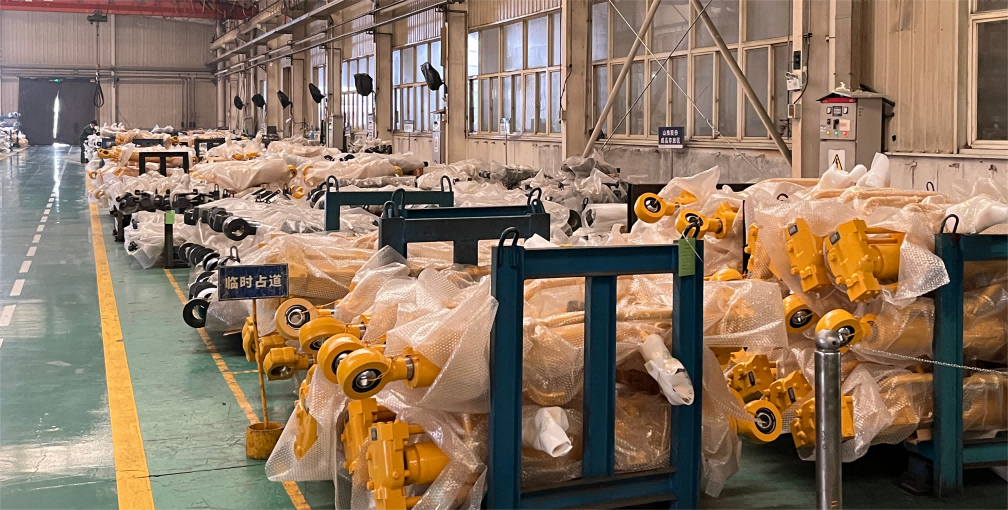
Finished cylinders are protected with anti-rust treatment, protective caps and export-grade packaging before shipment.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.